Tool Maintenance
6 min readSeptember 12, 2026Troubleshooting CNC Chatter: How to Eliminate Surface Ripples & Harmonics
Harmonic resonance between the machine frame, spindle RPM, and tool overhang ruins surface finishes. Use this diagnostic flowchart to quiet your CNC.
Amit Desai
Quality Assurance Director
#Chatter#Defects#Vibration#Spindle Care
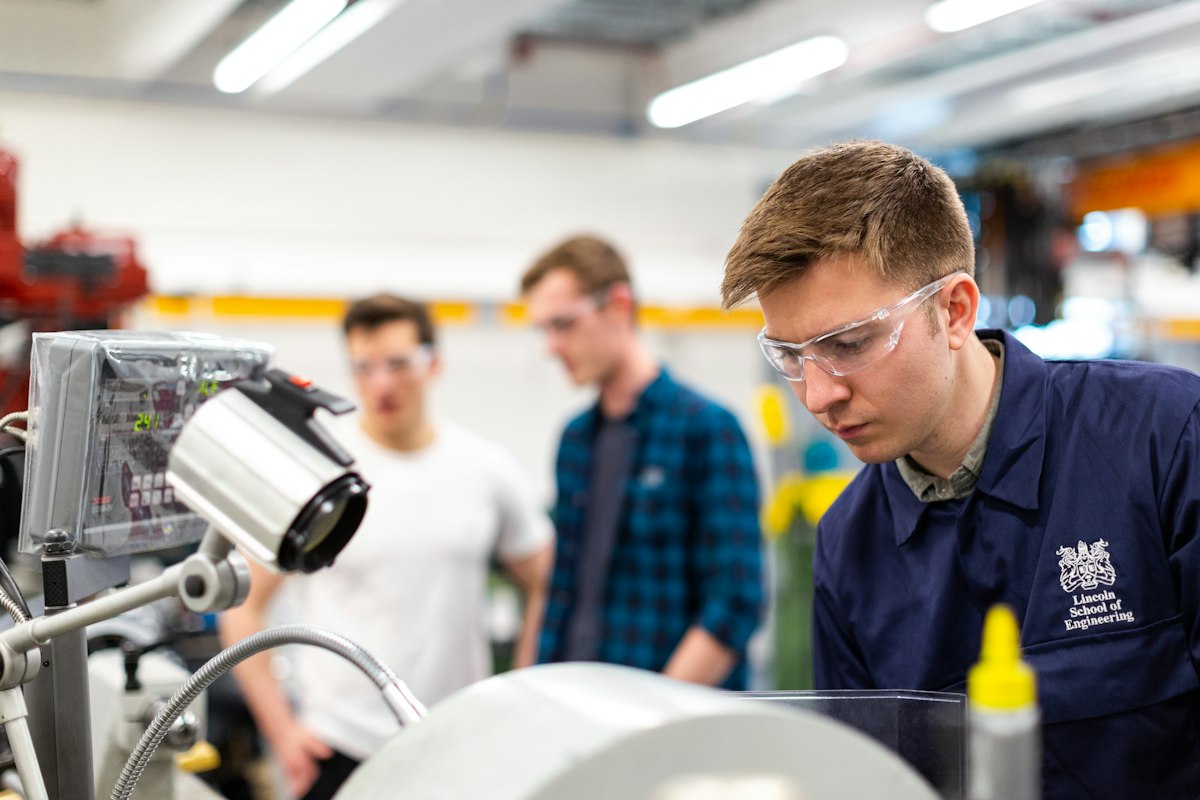
Understanding Chatter: Forced vs. Self-Excited Vibration
Chatter occurs when the natural harmonic frequency of the CNC machine resonates with the tooth-pass frequency of the rotating end mill. This creates microscopic surface waves that repeat across the workpiece.
Diagnostic Action Checklist
- Shorten Tool Stickout: Tool deflection increases with the cube of the overhang length (L³). Choking up the tool in the collet by just 6mm increases stiffness by over 50%.
- Adjust Spindle RPM by ±10%: Changing RPM shifts the tooth engagement frequency out of the machine's harmonic resonance pocket.
- Switch to Unequal Index / Variable Helix: Variable pitch flutes break the rhythm of harmonic resonance by ensuring each tooth impacts the material at a slightly different microsecond interval.
Remember that the CNC tooling industry is competitive, so standing out with high-quality products, excellent customer service, and innovation will be key to your success. If you’re looking for specific advice or information on certain aspects of manufacturing CNC router tools, feel free to ask!
Continue Learning
View All Guides